
 English
 Italian
 Spanish
 Thai
 Japanese
 Portuguese
 Korean
 Russian
 French
 German
 Polish
 Arabic
 Indonesian

Manufacturing Capability, Technical Evaluation, and Supplier Qualification
Selecting a 2-Bromo-1-[4-(methylsulfonyl)phenyl]-1-ethanone pharmaceutical intermediate supplier China involves more than comparing quotations and lead times. The supplier must be able to demonstrate that its manufacturing capabilities, analytical resources, quality controls, and documentation practices align with the customer's material requirements. For pharmaceutical intermediates, an attractive price is of limited value if the material cannot be qualified reliably or if inconsistent supply creates problems in downstream manufacturing.
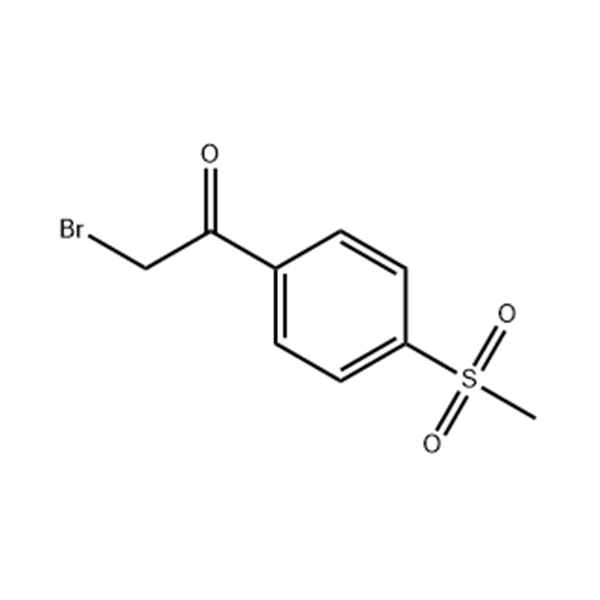
A structured supplier evaluation helps identify these risks before they affect a project. It also provides a practical basis for comparing manufacturers with different production models, technical resources, and levels of process integration. The most useful assessment focuses on verifiable capabilities rather than broad claims about quality, experience, or manufacturing scale.
Start With Product-Specific Manufacturing Capability
The first step is to confirm that a supplier can manufacture or reliably supply the exact compound required. A company may have extensive pharmaceutical experience without necessarily having an established process for every intermediate in its product portfolio. General chemical manufacturing capability should therefore be distinguished from demonstrated product-specific capability.
2-Bromo-1-[4-(methylsulfonyl)phenyl]-1-ethanone is a brominated aromatic ketone. Its molecular structure and the requirements of the customer's downstream process determine the relevant manufacturing and quality considerations. The supplier should be able to clarify whether the product is manufactured in-house, produced through a qualified external partner, or sourced through a trading arrangement.
This distinction matters because the organization responsible for the commercial transaction may not be the organization controlling the manufacturing process. A trading supplier may offer useful market access and logistics support, but the customer may need additional information about the actual manufacturing site, quality responsibilities, and traceability arrangements.
For direct manufacturers, a technical discussion should establish the maturity of the manufacturing process, the available quality controls, and the extent to which the proposed commercial material can be supported by documented manufacturing and analytical records. Where confidential manufacturing details cannot be disclosed, the supplier should still be able to provide sufficient information to support appropriate qualification.
Evaluate Process Engineering and Scale-Up Readiness
Manufacturing capability cannot be measured by facility size alone. Equipment suitability, process control, material handling, analytical monitoring, and the ability to manage deviations are all relevant when evaluating a pharmaceutical intermediate manufacturer.
Scale-up is particularly important when a project moves from laboratory development to routine production. Conditions that produce acceptable material in a small experiment may require further evaluation when equipment geometry, heat transfer, mixing, mass transfer, or work-up operations change. The degree of risk depends on the actual process, and it should be addressed through appropriate development and validation activities.
For a compound such as 2-Bromo-1-[4-(methylsulfonyl)phenyl]-1-ethanone, customers should avoid assuming that the presence of a brominated functional group automatically proves a particular process risk or manufacturing difficulty. Instead, the supplier should explain the relevant controls for its own process, including how it manages critical operating parameters, product isolation, impurity control, and batch release.
A manufacturer's equipment portfolio can provide useful evidence of technical breadth. Capabilities in high-temperature and high-pressure reactions, hydrogenation, chiral synthesis, or high-vacuum distillation may demonstrate experience with specialized pharmaceutical manufacturing operations. However, these capabilities should be interpreted in context. Their presence does not automatically establish that a specific intermediate uses those technologies or that every process step is performed at the same site.
The practical question is whether the supplier's available equipment and technical team are appropriate for the product and its required production scale. This should be confirmed through product-specific discussion and, where applicable, an audit or technical assessment.
Review Analytical Infrastructure Before Comparing Quotes
A supplier quotation should be evaluated alongside the analytical evidence that will support product release. A stated purity value is meaningful only when the test method, specification, and reporting basis are understood.
HPLC may be used to assess chromatographic purity and related substances, while NMR, mass spectrometry, or other suitable methods may support identity confirmation. The exact analytical package depends on the agreed specification and the customer's quality requirements. Additional tests may be necessary when a known impurity, residual solvent, or other material attribute presents a relevant risk.
During initial evaluation, customers should request a representative certificate of analysis and the current product specification. These documents help clarify whether the supplier reports actual batch results, whether limits are defined for each test, and whether the test methods appear appropriate for the intended application.
It is also useful to distinguish routine testing from additional testing available on request. A supplier may have access to advanced analytical instruments without conducting every possible test on every production batch. Customers should establish which tests form part of routine release, which are performed periodically or during qualification, and which require a separate agreement.
This approach prevents two common sourcing problems. The first is comparing suppliers whose purity figures are based on different analytical approaches. The second is assuming that a test will be performed simply because the supplier has the necessary equipment.
Assess Quality Systems and Regulatory Documentation
Pharmaceutical intermediate sourcing requires careful review of quality management practices. Company-level certifications, manufacturing licenses, and product-specific documentation serve different purposes and should not be treated as interchangeable.
An ISO 9001 certification relates to a quality management system within its stated scope. ISO 14001 addresses environmental management, while GB/T 45001 relates to occupational health and safety management. These certifications can provide useful evidence about the supplier's organizational systems, but they do not by themselves demonstrate that every product complies with every pharmaceutical requirement.
Similarly, a Drug Production License should be reviewed according to its applicable scope and the relevant regulatory context. Customers should confirm whether the proposed product and manufacturing activities fall within the arrangements represented by the supplier. If the project requires particular GMP evidence, customer audits, or additional quality documentation, those requirements should be discussed explicitly.
A complete qualification review may cover the product specification, certificate of analysis, safety data sheet, batch identification, packaging configuration, storage conditions, and quality contact arrangements. Depending on the customer's quality system, the process may also require a supplier questionnaire, audit, change notification agreement, or written quality agreement.
The objective is to establish a documented basis for accepting the material. It is not to accumulate certificates without determining whether they address the actual requirements of the project.
Examine Supply Reliability and Commercial Readiness
A qualified product is only one part of a successful sourcing arrangement. The supplier must also be able to provide realistic delivery commitments, clear order communication, and adequate shipment documentation.
When comparing offers, customers should distinguish between sample availability, initial commercial production, and repeat-order capability. A supplier may be able to provide a development sample quickly but require additional time to schedule a larger order. These situations are not necessarily signs of poor performance, but the commercial implications should be made clear before a project commits to a production schedule.
The quotation should identify the product, specification, packaging, order quantity, price basis, and delivery terms. It should also clarify whether analytical documentation and any agreed additional testing are included. If the customer requires a specific batch size, packaging format, or shipping arrangement, these requirements should be confirmed rather than inferred.
Supply reliability should be evaluated using evidence where available. Relevant indicators may include historical on-time delivery performance, the supplier's order planning process, its approach to raw-material availability, and its ability to communicate production changes. Claims about annual capacity should be interpreted carefully because total site capacity does not necessarily equal the available capacity for a particular compound.
For international customers, export documentation and shipment coordination are additional considerations. A supplier experienced in international trade may be better positioned to coordinate documentation and communication across markets, but the actual requirements for each destination should still be confirmed.
Why Manufacturer Experience Matters
An established pharmaceutical manufacturer can offer advantages in technical communication, process development, quality documentation, and long-term supply coordination. However, years in business should be treated as supporting evidence rather than a substitute for product-specific qualification.
Jiangsu Jingye Pharmaceutical was founded in 1994 and restructured in 2016. Its integrated operations cover research and development, production, and international trade. The company operates across a 50,000-square-meter site in Changzhou and maintains technical capabilities in high-temperature and high-pressure reactions, hydrogenation, chiral synthesis, and high-vacuum distillation.
The company reports compliance with GMP standards in its operations and maintains modern manufacturing facilities, analytical instruments, and an EHS system. Its credentials include a Drug Production License, ISO 9001, ISO 14001, and GB/T 45001 certifications. It also reports long-term cooperation with universities and research institutions and exports products to Europe, the Americas, Southeast Asia, Japan, and South Korea.
For customers evaluating Jiangsu Jingye Pharmaceutical as a potential partner, these details provide a starting point for technical and organizational assessment. They do not, on their own, establish that the company currently manufactures the specific compound in question or that a particular order can be fulfilled within a given period. Product availability, manufacturing responsibility, specifications, and delivery conditions should be confirmed directly.
Use a Risk-Based Supplier Qualification Process
An effective supplier qualification process begins by defining what the material must achieve. This includes the required identity, purity, impurity limits, testing methods, packaging, storage conditions, and documentation.
The next step is to compare suppliers against the same requirements. If one supplier offers additional testing or a different packaging configuration, the difference should be recorded clearly. This makes it easier to determine whether a price difference reflects a genuine difference in scope or simply a different commercial offer.
Sample testing can help establish whether a proposed material meets the agreed specification. For projects progressing toward routine use, further assessment may be appropriate to evaluate batch consistency, production controls, and documentation reliability. Where the application is subject to formal qualification requirements, the process should follow the customer's applicable procedures.
Communication should also be assessed during qualification. A supplier that responds precisely to questions about specifications, test methods, batch records, and delivery assumptions provides a stronger basis for a long-term relationship than one that relies exclusively on generic marketing statements.
Conclusion
Choosing a 2-Bromo-1-[4-(methylsulfonyl)phenyl]-1-ethanone pharmaceutical intermediate supplier China requires a balanced assessment of manufacturing capability, analytical control, quality systems, and commercial readiness. Facility scale and company history can be relevant, but the decisive evidence is the supplier's ability to meet the agreed product specification and support a controlled supply process.
Jiangsu Jingye Pharmaceutical combines pharmaceutical manufacturing experience, specialized process capabilities, analytical resources, and international trade experience. Customers considering the company for this intermediate should verify product-specific availability, the applicable manufacturing arrangements, analytical documentation, and delivery commitments as part of their qualification process.
The most reliable supplier decision is one based on documented technical fit and realistic supply commitments, rather than a single purity figure or the lowest quoted price.